Great vision begins with one aim – to open new possibilities for better outcomes.
At Shah Eye Care, this belief guides our approach to ophthalmic medical device manufacturing. Founded in 2010 as part of the Shah Group of Companies, we have grown from a focused ophthalmic device manufacturer into a global partner serving customers across 80+ countries.
With more than 25 million ophthalmic blades supplied worldwide, our journey is built around precision, quality and continuous development.
Manufacturing Built for Precision and Quality
Shah Eye Care operates with modern manufacturing infrastructure, qualified teams and controlled production environments in southern India. Our ISO Class 7 cleanrooms support precision manufacturing and assembly, while dedicated quality, regulatory, warehousing and operational teams maintain control throughout the production process.
Automation is an important part of our manufacturing approach. Automated electro-etching, assembly, in-process inspections and packaging help improve consistency, precision and production efficiency. Our manufacturing capabilities also incorporate German-adapted technology and machinery.
MDR Certified Ophthalmic Surgical Devices
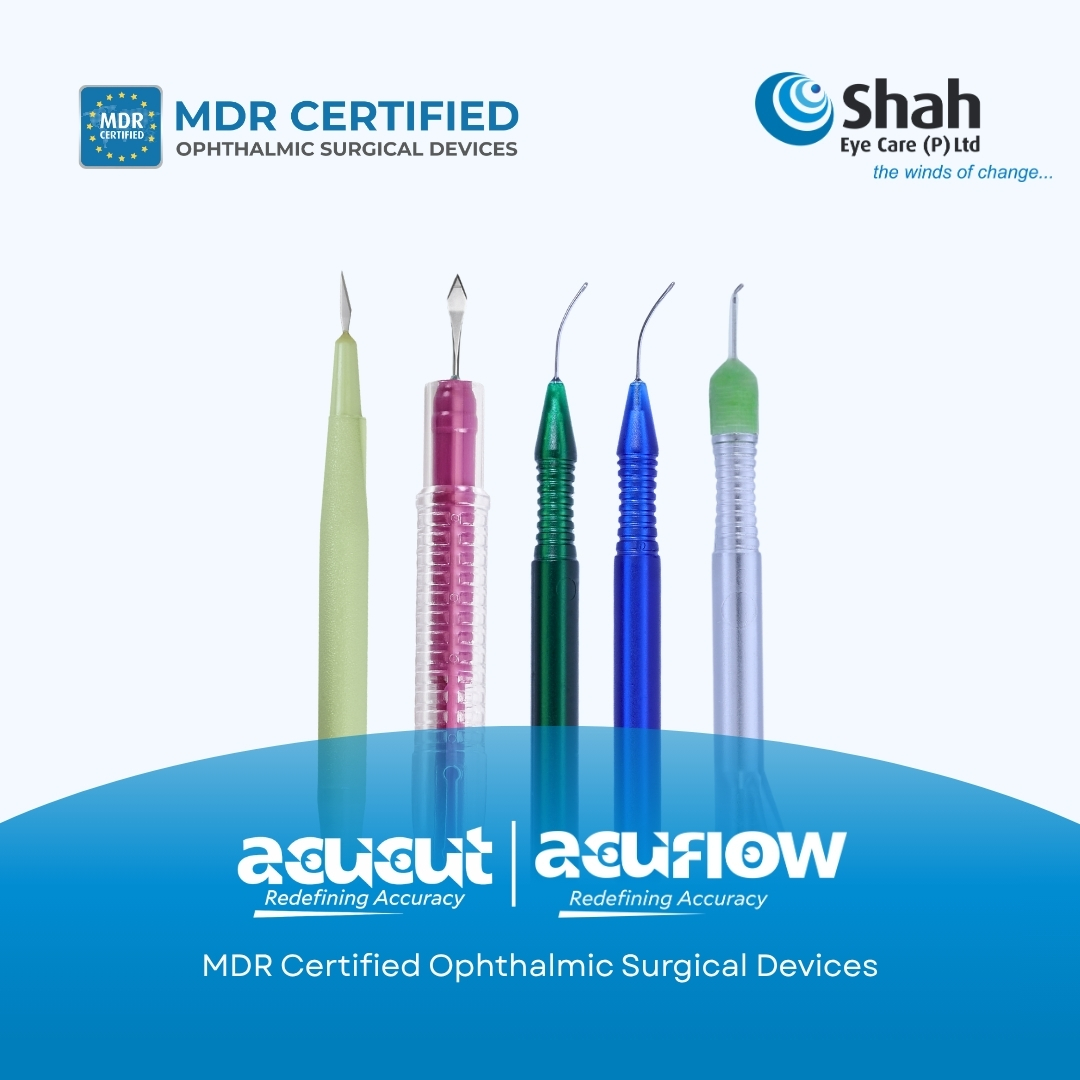
We demonstrate our focus on quality and regulatory requirements through our portfolio of MDR Certified Ophthalmic Surgical Devices.
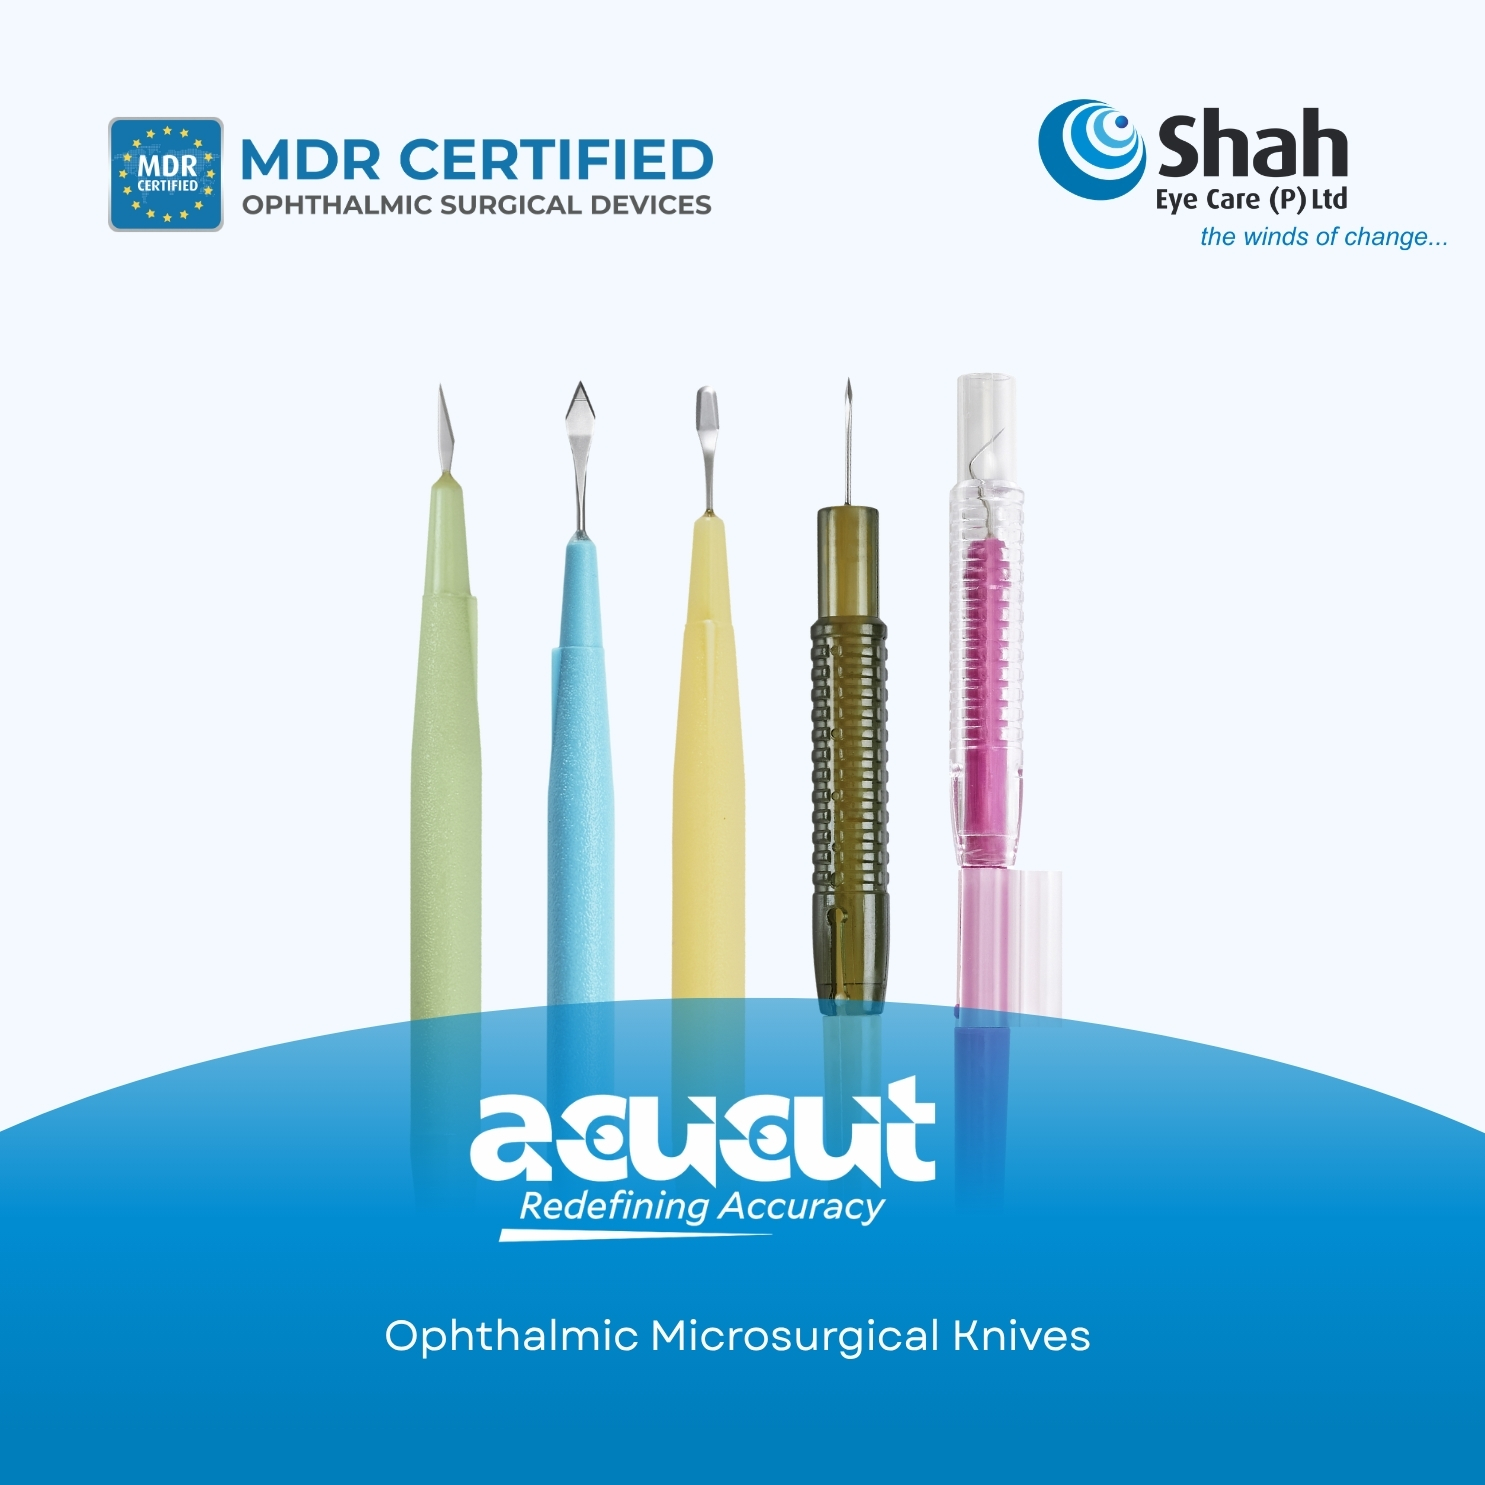
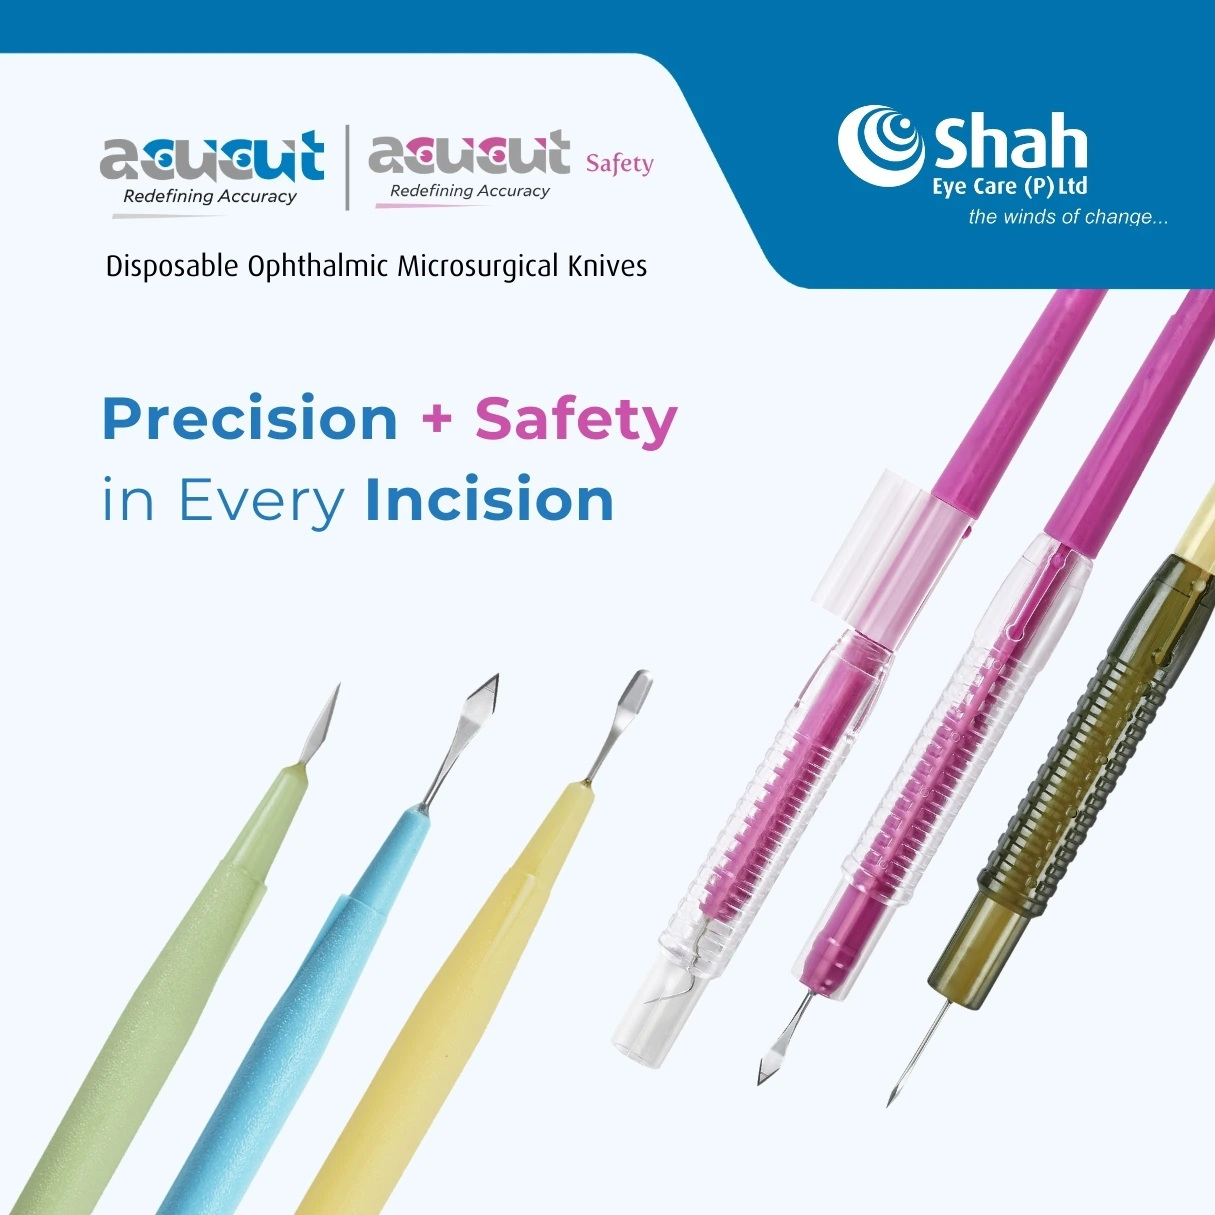
The ACUCUT and ACUCUT SAFETY ranges are MDR-certified ophthalmic microsurgical knives manufactured through controlled and monitored processes.
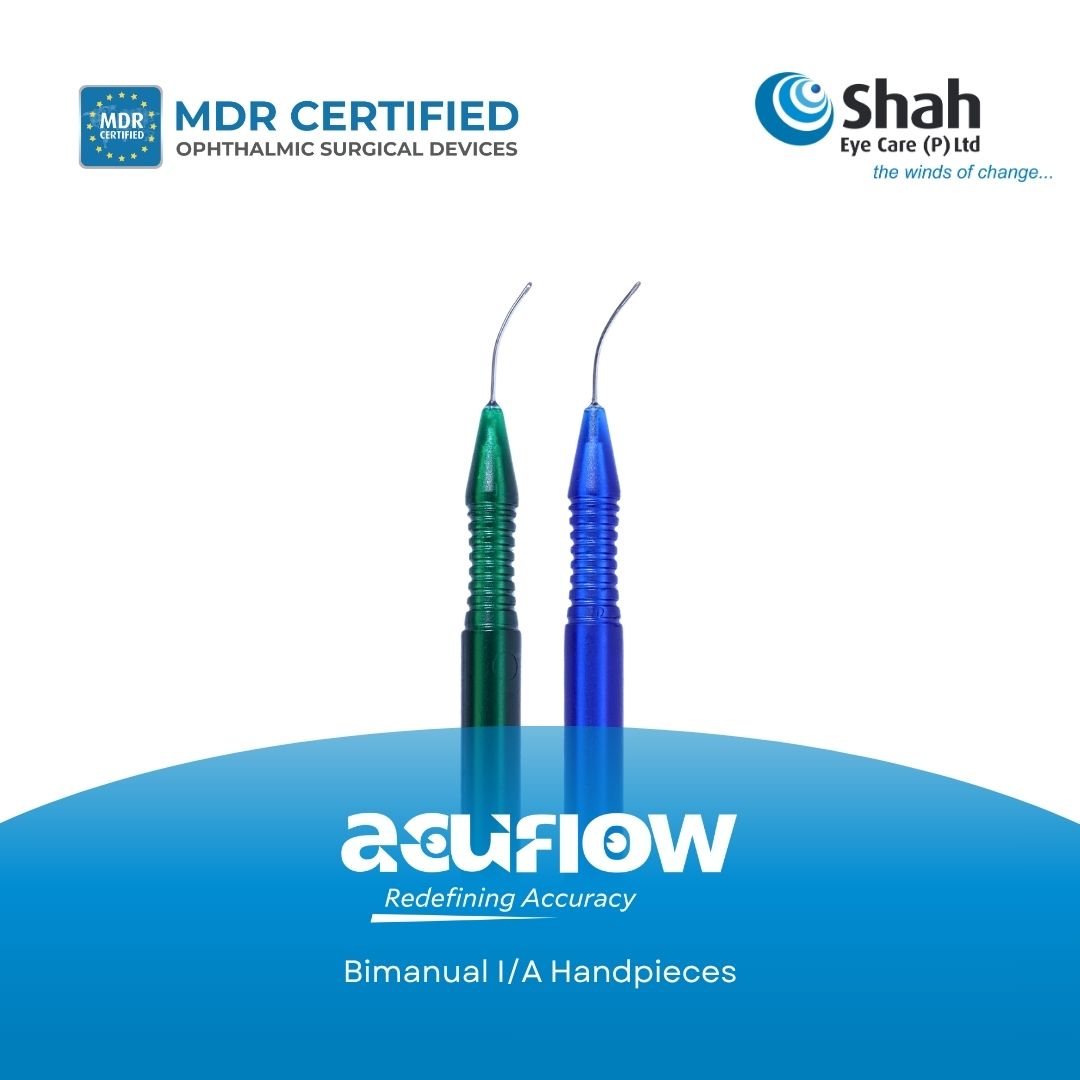
Our portfolio also includes ACUFLOW, an MDR-certified range of Bimanual and Coaxial Irrigation and Aspiration (I/A) Handpieces. Manufactured in controlled facilities, ACUFLOW is designed to support controlled fluid management during ophthalmic procedures.
Together, these products represent our expanding capabilities across different stages of ophthalmic surgery.
Expanding Our Ophthalmic Product Portfolio
Our development journey continues with ShahVisc, our upcoming range of ophthalmic viscosurgical devices.
ShahVisc combines Swiss technology with hyaluronic acid-based formulations and follows controlled processes for formulation, filling, sterilisation, and packaging.
Beyond our own brands, we also work with ophthalmic companies through OBL and Private Labelling, providing customised solutions based on specific product and market requirements.
End-to-End Manufacturing and Regulatory Support
Our capabilities extend across the complete product development and manufacturing journey – from research, design and prototyping to manufacturing, assembly, testing, packaging and final product realisation.
Our quality and regulatory teams work closely across these stages, managing documentation, traceability, validation, stability studies and customer audit requirements.
We also collaborate with reputed laboratories for essential testing, including sterilisation, biocompatibility and material evaluation. This integrated approach helps us maintain quality and regulatory control throughout the product lifecycle.
From India, for the World
Behind every product is a team working across production, quality, regulatory, supply chain, research and product development, warehousing, finance and marketing.
Together, these teams support our goal of delivering consistent products and building long-term relationships with customers and partners worldwide.
With modern manufacturing infrastructure, regulatory expertise, automation and an expanding ophthalmic portfolio, Shah Eye Care continues to develop solutions for the evolving needs of global ophthalmic markets.
Shah Eye Care – From India, for the world.
Discover more on our website: https://shaheyecare.com/
Visit our LinkedIn page: https://in.linkedin.com/company/shah-eye-care